Semiconductor Fabs Move Yield Detection Closer to the Process—and Strain Data Systems
- Gate
- AI & ML
- Departs
- Crew
- Anne Meixner and Laura Peters
- Passengers
- 803
Real-time sensor analytics can catch process drift sooner, but fabs need richer data links and context to make module-level AI useful across production.
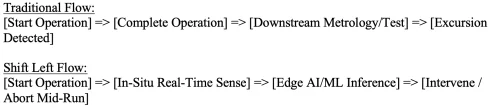
Moving yield detection into the process module can shorten the gap between a manufacturing fault and a corrective action. The tradeoff is a much harder data problem: fabs must capture and analyze increasingly dense equipment signals in near real time, while preserving enough context to connect results across tools and process steps.
That tension is becoming more pronounced as semiconductor manufacturers apply AI and machine learning to equipment data. Some fabs collect hundreds of petabytes of data a year, according to the source article, while higher sampling rates and raw sensor traces add to the volume. The aim is practical: identify process drift before it affects later steps, then adjust a tool or stop a run rather than wait for downstream screening to reveal a yield problem.
More data, at higher speed
Equipment data has grown sharply over the past five years, said Ashish Gupta, senior data engineering manager for automation at Intel Foundry. He linked that increase to fabs moving process control into real-time, in-situ monitoring.
Jae Yong Park, vice president of enterprise software business at Onto Innovation, described three drivers: equipment suppliers have added hundreds of parameters; sampling has advanced from roughly once per second to intervals of tens of milliseconds; and engineers increasingly work with raw traces rather than summaries. The combined effect is a larger and faster stream with more varied signals.
For some applications, analysis must happen in less than a second. The number of sensor types in use has also increased the variety of data substantially compared with a decade ago. Collecting those signals is only part of the challenge. A fab needs to decide which measurements are useful, move them to the right software, and process them quickly enough to inform an action while the tool is still running.
Some equipment generates signals at rates that make full capture impractical. Kartik Venkataraman, senior director of product management at Synopsys, pointed to RF plasma sources in etch and chemical vapor deposition chambers. A source may operate at megahertz frequencies, while pulsing can occur at kilohertz rates. Each pulse has a waveform with features such as transient response and droop, some of which might reveal process conditions. Capturing every waveform could mean megabytes of data per second, he said, beyond what a fab can readily monitor.
Access is another constraint. Venkataraman said fabs may see only a fraction of the data generated by equipment. Some information remains with equipment makers as proprietary know-how; in other cases, the fab lacks the capacity to handle it. This means the question is not simply whether a sensor can produce a signal. It is whether the signal can be accessed, interpreted, and acted on at the required speed.
From downstream screening to in-module decisions
Traditional yield learning can take days, weeks, or months, as problems emerge through later inspection or electrical testing. Shifting detection upstream lets a fab use sensor data and virtual metrology models to identify a potential excursion within the process module. An inference model can flag a wafer for review, trigger a change to equipment settings, or prompt the process to stop. If the run is halted, engineers can investigate the cause and decide on corrective work, including maintenance.
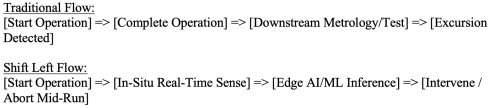
Fig. 1: Shift left identifies yield excursions earlier and better supports advanced process control. Source: Intel Foundry
This is an extension of a longer shift in semiconductor testing. Test content has moved toward wafer-level screening to improve the likelihood that good die reach later stages. The rise of chiplets has added testing of singulated die, helping manufacturers check known-good die before assembly. In the fab, the corresponding change is to use equipment data earlier, before later screening steps expose the impact of a process deviation.
Gupta said earlier detection can happen within several phases of the manufacturing flow, but moving it inside a fab module, design cycle, or test cell intensifies the data engineering work. Instead of relying on summary results or post-step inspection, teams need continuous high-resolution monitoring, anomaly detection, in-situ analytics, virtual metrology, and adaptive control. Those uses put pressure on data volume, velocity, variety, and veracity—the reliability and meaning of the information being analyzed.
The same logic applies to plant conditions around a tool. Water temperature and pressure, as well as power fluctuations, can affect processing. Steve Zamek, director of product management at PDF Solutions, argued that data from equipment below the main fab floor can also support near-real-time analysis. The operating conditions of connected components can influence the material processed by a tool, so excluding them may leave a model with an incomplete view.
Virtual metrology adds another route to earlier decisions. Rather than waiting for a direct measurement that may arrive later, a model estimates a product-quality metric from equipment parameters. Zamek said software can detect faults and intervene before more material is scrapped, particularly when the model can accurately predict a quality measure that cannot be observed in situ. The value depends on the model’s predictive quality; a fast estimate is useful only if teams can trust it.
AI needs more than summary data
Many existing process-control systems rely on summary measurements and statistical process control. AI and machine-learning inference can work with richer traces and more varied inputs, supporting chamber analysis, anomaly detection, and virtual metrology. Onto Innovation’s Prasad Bachiraju, senior director of sales and product marketing, said fabs are using raw trace data for outlier detection and root-cause analysis to find signals that conventional statistical methods might miss.
Intel Foundry’s Gupta also linked upstream defect detection to more frequent inspection, denser metrology sampling, and measurements at more locations across a wafer. Better sensor fidelity and new measurement types can feed more detailed models for process control and anomaly detection. That creates an important distinction: AI does not remove the need for measurement infrastructure. It can increase demand for both the underlying signals and the checks used to validate model output.
Potential gains extend beyond yield. Jon Holt, senior director of product management at PDF Solutions, said models can identify patterns across operational, process, and equipment data that are difficult to spot manually. In principle, that can help teams anticipate quality problems, reduce process variation, speed root-cause work, and support predictive maintenance. These are intended benefits, not automatic outcomes: they depend on useful data, well-calibrated models, and a path from model output to a production decision.
Conventional inspection, metrology, and test still matter. They catch issues that inference models miss and provide feedback that can improve those models. This makes an architecture focused only on local, real-time decisions incomplete. A module may respond quickly to its own signals, yet the fab still needs traceable records connecting those signals to what happened before and after the operation.
The cost of local optimization
Data access and standardization are central to that connection. Equipment logs need to reach process engineers who build and monitor models. Bachiraju said equipment suppliers should export relevant data in standard formats and pass information about what happened to a wafer or panel to the next step. That gives the following process a chance to use the history rather than treating each operation as an isolated event.
In practice, teams often optimize data handling for the immediate constraints of one process module. Gupta described the result as “data rich but context poor”: a module may have high-resolution information for its own decisions while enterprise integration and cross-module traceability receive less attention. That can make it harder to correlate process conditions with later outcomes or to reuse learning across tools.
The paradox is that local inference models need connected data, too. Their performance must be checked against downstream results, and their training data needs enough provenance to explain what a measurement represents. If teams use different local definitions or fail to retain links between steps, combining records becomes harder. The result can be siloed models that work within narrow boundaries but struggle to support broader process learning.
There is no easy starting point for a mature fab with years of separate systems and data conventions. Jim Schiely, chief of staff for Calibre Semiconductor R&D at Siemens EDA, said new large-scale manufacturing ventures have an opportunity to build shared data structures from the outset. Rather than creating separate local models and records for each department, teams could establish connections among data types and their origins. He described those connections as a graph that AI systems can draw on.
Established fabs face a different task: updating modeling practices and data systems that were built when model development was more manual. Schiely recalled that lithography modeling once depended on a small number of specialists who could make difficult data sets work. Computing resources and software libraries have since made automated model fitting, including neural-network approaches, more practical. But the effort to organize and maintain data only pays off if the data remains current and is used.
Models still need physical grounding
Digital twins and AI can help connect observations to process behavior, but they cannot replace the work of establishing what is physically true. Venkataraman said core simulation engines must generate the ground truth, with human expertise and real measurements used to validate and calibrate the models. Physical models describe expected behavior; production data anchors those expectations in actual conditions. A digital twin becomes more useful when it can help explain why observed data behaves as it does, rather than simply displaying a record of what happened.
That calibration requirement grows with device and packaging complexity. Russell Dover, managing director of equipment intelligence product development at Lam Research, cited gate-all-around logic devices, 3D DRAM, modular-stack NAND, and multi-die packages such as HBM and system-in-package designs. These processes make faster learning and problem resolution more valuable, while increasing the number of interactions engineers need to understand.
Dover described using feedback or feedforward from different tools to improve a connected manufacturing outcome. Data can also be compared across separate fabs, treating equipment in different locations as a virtual fleet. That extends tool matching beyond chambers in one facility and may help teams improve process output across a wider set of equipment. The practical challenge is making sure records from different sites are comparable and carry enough context for a meaningful comparison.
Plasma processing shows why context matters. Shalini Sharma, head of semiconductor materials innovation and cross-vertical strategy at SandboxAQ, said residue on chamber walls can change gas-phase chemistry and shift etch rates as a chamber ages. Engineers use designed experiments, chamber telemetry, and witness wafers to characterize those effects, then manage them through cleaning, seasoning, and run-to-run control. Machine learning can identify relationships among RF impedance, gas flow, and other sensor signals; virtual metrology can estimate film thickness or etch depth before conventional measurements arrive.
That example also points to what fabs should watch next: not just whether models can make faster predictions, but whether the data pipeline preserves tool state, process history, and measurement provenance. Shifting detection into the module can reduce the wait for a yield signal, but it doesn't make downstream checks or cross-step data links optional. The strongest case for real-time AI is likely to come from systems that pair fast local action with traceable, calibrated learning across the fab.
— Ed Sperling contributed to this article.
Related Articles
How Robotics And Intelligent Equipment Control Drive Next-Gen Fab Productivity
Advanced equipment control and robotics can improve repeatability, tool uptime, and yield.
Secure Data Sharing Becoming Critical For Chip Manufacturing
Data sharing is increasingly relevant to advanced devices and multi-die assemblies.
Digital Twins: The Cloud’s The Limit
The chip industry uses large-scale computing and AI for virtual test environments.
New Frontiers In Fault Detection And Classification
AI can support timelier, more accurate data, while automated equipment control remains a further step.
The post Shift Left Complicates Fab Data Management appeared first on Semiconductor Engineering.


